


Home » Vietnam News » Tsubaki Neptune Chain: The Ultimate Drive Solution for High-Moisture and Chemical Environments
Tsubaki Neptune Chain: The Ultimate Drive Solution for High-Moisture and Chemical Environments
High humidity and continuous chemical washdowns cause standard steel chains to rust quickly. To completely solve this corrosion issue without interrupting your production lines, Tsubaki Neptune Chain stands out as the superior corrosion-resistant solution. Combining advanced surface coating technology with the mechanical strength of carbon steel, it helps processing and packaging systems operate reliably while optimizing overall efficiency.
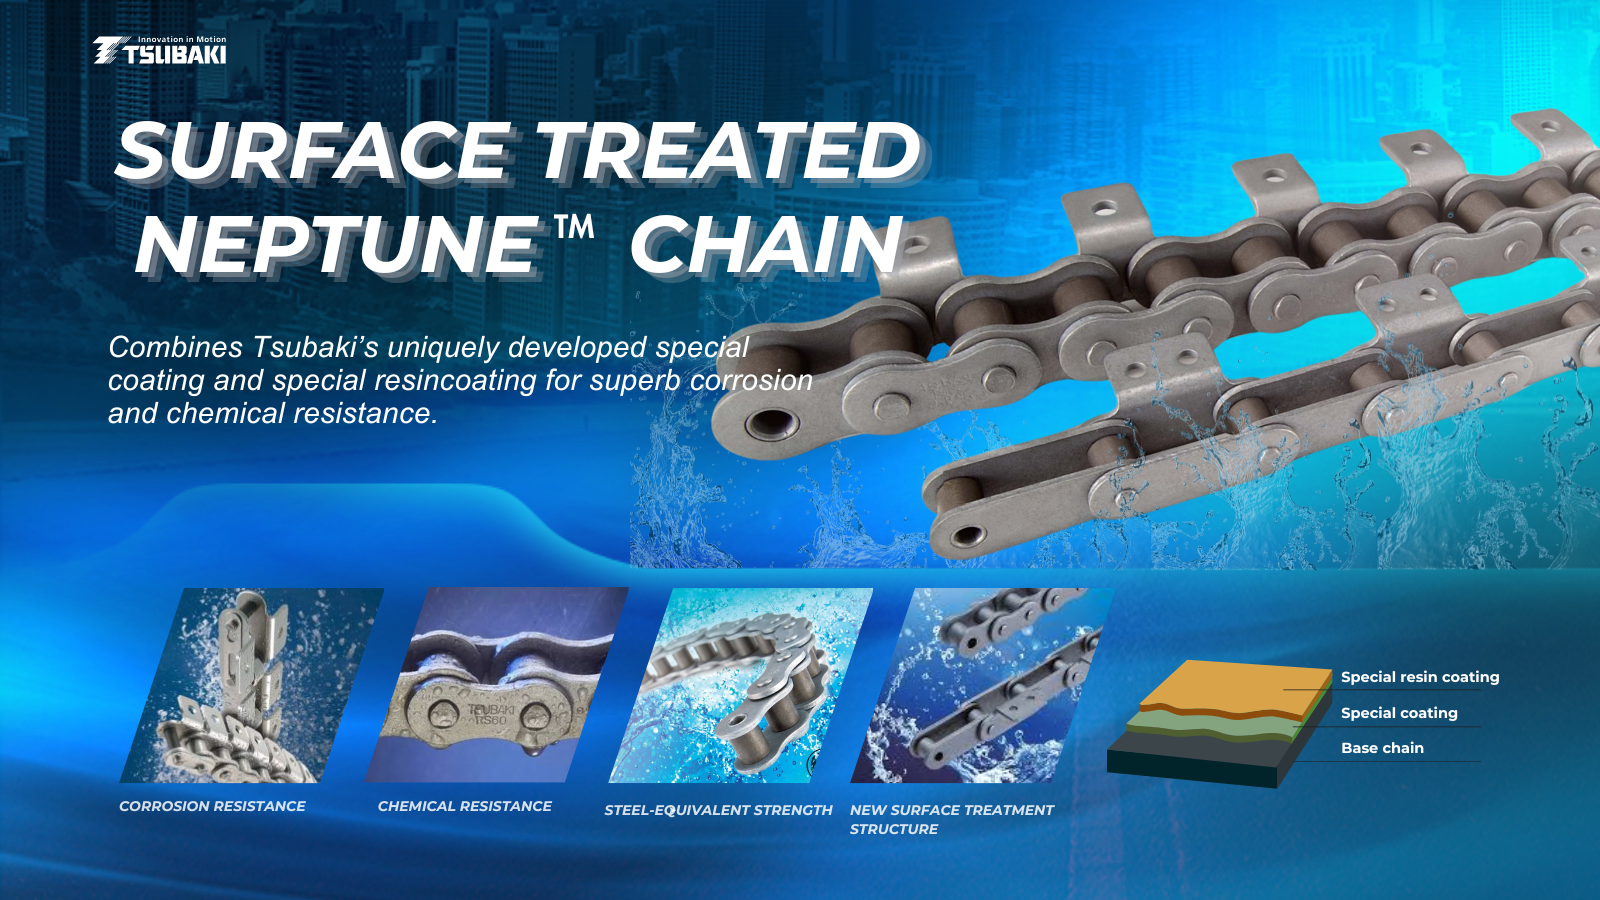
Advanced 2-Layer Coating Technology of Tsubaki Neptune Chain
-
Full carbon steel strength: Unlike conventional coated chains, Tsubaki's treatment technology ensures that the maximum allowable load and minimum tensile strength are not compromised compared to standard carbon steel chains.
-
RoHS-compliant safety: Free from hexavalent chromium (Cr6+) as well as hazardous heavy metals such as lead and mercury.
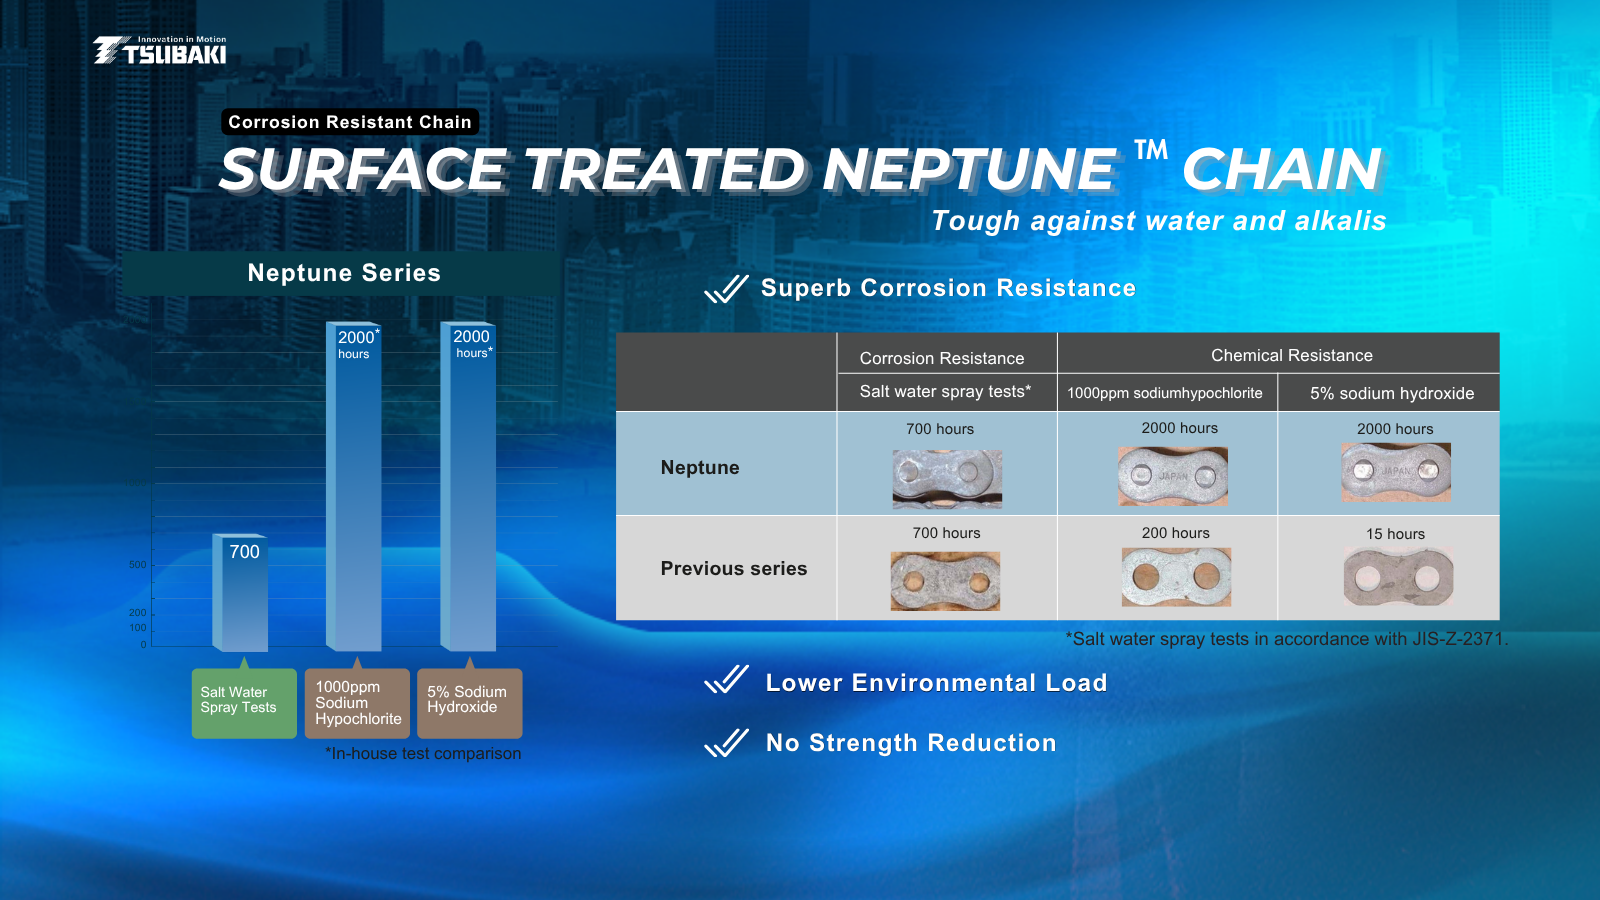
Advanced 2-layer coating: The chain surface is protected by a special coating combined with a special resin coating, delivering optimal resistance against moisture, salt water, and harsh detergents.
Practical Applications of Tsubaki Neptune Chain in Manufacturing
Thanks to its exceptional durability in harsh conditions, Neptune Chain is widely used across various systems:
-
Food processing & packaging lines
-
Sterilization & freezing conveyors
-
Environmental treatment systems & automated warehouses
Whether you are handling facility maintenance, system engineering, or equipment procurement, our Tsubaki technical team understands the risks you face--and we're ready to partner with you to ensure your production lines keep moving smoothly.
Contact Tsubakimoto Vietnam today for expert advice on the Neptune drive chain solution best suited to your plant's technical requirements!
Website: tsubaki.net.vn
Email: sales@tsubaki.net.vn
Fanpage: Tsubakimoto Vietnam